

Carbon Fiber Solutions for LNG and Cryogenic Facilities: Beating Thermal Cycling and Corrosion
- 2026-10-05
Why Steel Keeps Failing in LNG Service — and What Actually Sensible Material Engineers Do About It
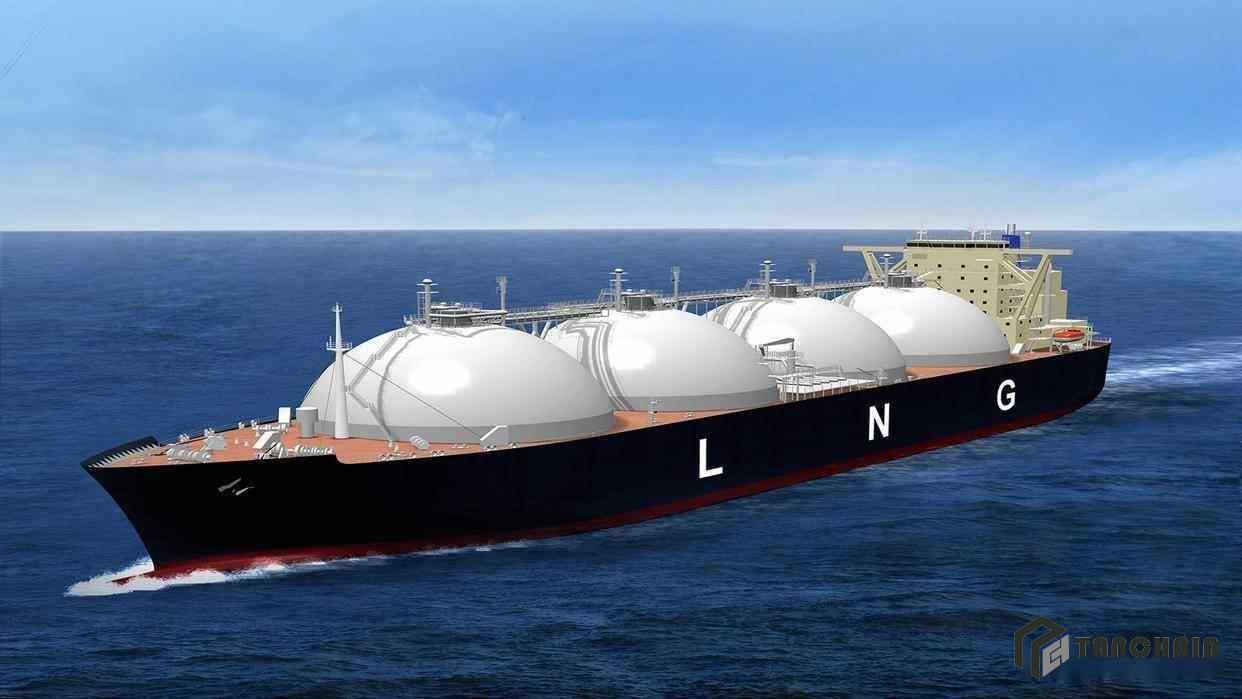
Ask anyone who has walked an LNG export terminal at midnight why structural components keep getting redesigned, and you will rarely hear "because of corrosion" first. The honest answer is thermal cycling. A piping support that sits at -162 °C during a transfer campaign and then warms back toward ambient is not just cold — it is being stretched and compressed, thousands of times, by its own contraction. Steel handles the load; it does not handle the motion that comes with it.
The second answer is condensation. Any bare carbon steel surface below the dew point of the surrounding air pulls water out of that air, continuously, and that water arrives with chlorides in it if the site is coastal. The combination — cyclic thermal strain plus chloride-laden condensate — is a corrosion-fatigue environment that no standard coating schedule survives indefinitely.
This is the problem this solution addresses. It is not a "carbon fibre is strong" article. It is a practical account of how composite materials — carbon fibre laminates, pultruded and filament-wound carbon fibre tube, and aramid reinforcement — replace the parts of an LNG facility that steel keeps losing, and what an engineer needs to know before specifying them.
The Real-World Problems: Four Failure Modes We See Repeatedly
Before listing products, it is worth naming the specific problems the composite solution is answering. Vague problem statements produce vague material selections, and LNG work is unforgiving of vague selections.
① Thermal Contraction and the Stress It Leaves Behind
Stainless steel contracts roughly 2.6 mm per metre between ambient and liquefied-gas temperature. Across a long run of pipe or a large insulated structure, that adds up to centimetres of movement that must be absorbed somewhere — usually in expansion loops, sliding shoes or bellows, each of which is a maintenance item. Components that themselves have a much lower coefficient of thermal expansion reduce the total movement the structure has to tolerate.
② Condensation, Ice and Corrosion Under Insulation
Cold-bridge components — support shoes, hangers, brackets, clamps — are the classic weak points. They penetrate the insulation system, they sit cold, and they collect moisture. Corrosion under insulation (CUI) on these parts is one of the most expensive inspection findings in a cryogenic plant because it is hidden and slow until it is structural.
③ Vibration From Compressors and Pump Skids
LNG trains run large reciprocating and centrifugal machines. Structural resonance in their local supports is not a theoretical concern; it is a routine source of cracked welds and loosened fasteners. Material damping matters as much as stiffness here.
④ Weight, Access and Installation Cost
Offshore and remote-train facilities pay for every kilogram twice: once in shipping, once in the crane time and man-hours needed to install it. Components that can be carried by two people instead of lifted by a crew change the schedule and the cost of every campaign.
How Carbon Fibre Composites Solve the LNG Material Problem
The solution uses three core composite forms, each chosen because it answers one or more of the failure modes above. None of them is a universal replacement for steel; each wins in a specific, well-defined role.
Carbon Fibre Laminates and Prepreg for Cold-Bridge and Load-Bearing Parts
Carbon fibre reinforced polymer (CFRP) has a coefficient of thermal expansion roughly an order of magnitude lower than steel along the fibre direction, and it does not corrode in the chlorides that coastal sites bring with them. For structural spacers, cold-bridge blocks, support inserts and reinforcement plates, this eliminates the two simultaneous drivers of failure: differential expansion and corrosion under insulation.
Our carbon fibre prepreg — resin pre-impregnated woven fabric and unidirectional tape — gives the part its structural capacity, and our carbon fibre fabric provides the surfacing layers where impact or abrasion resistance is needed. Because the laminate can be layed up with the fibre axis aligned to the actual load path, stiffness is placed where the structure needs it rather than where a stock steel section happens to put it.
Pultruded and Filament-Wound Carbon Fibre Tube for Supports and Handrails
Where the component is long and slender — pipe supports, standoffs, platform handrails, ladder rails, secondary structural members — carbon fibre tube is the practical form. Pultruded tube gives a constant cross-section at a competitive cost per metre; filament-wound tube is chosen where hoop strength or a tuned winding angle is required.
The value in cryogenic service is twofold. First, lower thermal conductivity than steel means the tube itself acts as part of the thermal break, reducing the cooling load that the insulation system has to manage. Second, the tube does not rust, pit or need repainting, which removes it from the CUI inspection list entirely.
Aramid Reinforcement Where Impact Protection Is the Priority
Aramid filament and aramid fabric bring impact and cut resistance that carbon fibre alone does not offer. On LNG sites these materials are used for protective wrappers, impact-resistant panels around loading areas, and protective covers where a purely carbon-fibre part could be damaged by a dropped tool or a bump from rotating equipment. Aramid also brings excellent damping, which is useful on supports that sit near machinery.
Pre-Oxidized Fibre for Fire and Thermal Protection Around Hot Ends
Even in a cryogenic plant there are hot zones: gas turbines, recondenser heat, compressor buildings, flare lines. Pre-oxidized fibre yarn, fabric and felt are inherently flame-retardant, non-melting and non-dripping, and are used for fire barrier blankets, duct lagging and insulation around equipment where a non-combustible barrier is required by practice or code.
Performance Basis: Why These Materials Behave the Way They Do
Every claim above has a physical basis, and it is worth stating them plainly so the selection is defensible in a design review.
Low thermal expansion — CFRP expands at roughly 1–2 × 10⁻⁶ /K along the fibre axis, compared with about 12 × 10⁻⁶ /K for steel. A 3 m carbon fibre support moves a fraction of the distance a steel one does over the same temperature swing, which directly reduces the travel the surrounding structure must absorb.
High specific stiffness — carbon fibre composite delivers the stiffness of steel at roughly a quarter of its density. For handrails, walkway supports and inspection platforms this means lighter members with the same rigidity, and less dead load on the structure they sit on.
Corrosion immunity — the polymer matrix and the carbon reinforcement are not subject to galvanic rusting in the way steel is. In chloride-bearing, condensation-prone environments this is the difference between a part that lasts the life of the plant and one on a five-year replacement cycle.
Vibration damping — composite laminates damp structural vibration significantly better than metals, which is relevant on any support near reciprocating compressors or pumps. Lower amplitude means lower fatigue accumulation at welds and fasteners.
Non-combustible protection from pre-oxidized fibre — pre-oxidized (stabilized) fibre does not melt or drip and provides a stable, flame-retardant barrier at high ambient temperatures, which is why it is used for fire blankets and equipment insulation in industrial settings.
Selection Matrix: Which Carbon Fibre Product for Which LNG Component
The table below is deliberately a starting point, not a substitution for structural calculation. It maps the common cryogenic-site components to the material form that suits them, with the governing property indicated.
| LNG Component / Zone | Recommended Product | Governing Property |
|---|---|---|
| Cold-bridge support blocks and spacers | Carbon fibre board / CFRP laminate | Low thermal conductivity, low expansion |
| Pipe and rack support standoffs | Pultruded carbon fibre tube | Specific stiffness, corrosion immunity |
| Platform handrails and ladder rails | Filament-wound carbon fibre tube | Light weight, stiffness, durability |
| Structural reinforcement and repair plates | Carbon fibre prepreg + carbon fibre fabric | Strength, tunable fibre orientation |
| Impact and protection panels | Aramid fabric laminate / hybrid aramid-carbon | Impact and cut resistance, damping |
| Fire barriers and blanket around hot equipment | Pre-oxidized fibre fabric, felt, yarn | Flame retardance, thermal stability |
| Insulation lagging on warm pipework | Pre-oxidized fibre felt | Thermal insulation, non-combustible |
| Brackets, clamps and small fittings | Carbon fibre chopped-fibre compound | Weight reduction, part consolidation |
Implementation Notes From the Field
Getting the material right is only half the job. These are the practical points that decide whether a composite installation in a cryogenic plant performs as designed.
Fibre Orientation Follows the Load, Not the Drawing
Carbon fibre is strong and stiff along the fibre axis and comparatively weak across it. A laminate that is simply "made of carbon fibre" but oriented along the convenient axis will underperform badly. The lay-up must follow the real load path, and on load-bearing parts the fibre direction should be agreed with the design engineer before tooling is cut.
Isolate Carbon Fibre From Metal Fasteners
Carbon is cathodic relative to steel and aluminium, so direct metal-to-carbon contact at a bolted or riveted joint can drive galvanic corrosion of the metal — accelerated by the moisture and chlorides present at LNG sites. Use insulating washers, sleeves or glass-fibre isolating plies at every carbon-to-metal interface. This single detail prevents most field failures of composite structures.
Design the Thermal Break Deliberately
A composite support component reduces heat flow, but it does not eliminate it. Where the design requires a specific heat-leak limit, the component thickness and the number of insulation layers should be calculated rather than assumed. In practice, pultruded carbon fibre tube combined with a defined thermal break gives a predictable, inspectable result.
Choose the Manufacturing Route Early
Pultrusion is the economical route for constant cross-sections such as tubes and boards in quantity. Roll wrapping suits higher-performance tubes and thicker walls. Prepreg lay-up is used for complex or high-value structural parts where the lowest weight and highest stiffness matter. Making this choice at the concept stage avoids redesign later.
Plan Fire and Thermal Protection Together With the Structure
On combination-service sites — where cryogenic and hot zones sit in the same footprint — the flame and insulation requirement should be designed alongside the structural component, not added afterwards. Pre-oxidized fibre felt and fabric are supplied in the same programme as the structural carbon fibre products, so the assembly is qualified as one system.
The Material Forms We Supply for LNG and Cryogenic Projects
A single qualified source for the full range removes the compatibility risk that comes from mixing materials from different suppliers, and it shortens qualification at the start of a project.
Carbon fibre filament and tow — base material for winding and pultruding structural tubes and profiles.
Carbon fibre woven fabric — 3K and 12K weaves for laminates, surfacing and repair systems.
Carbon fibre prepreg — resin pre-impregnated fabric and unidirectional tape for the highest-performance structural parts.
Carbon fibre tube — pultruded and filament-wound, for supports, handrails and secondary structure.
Carbon fibre board — flat laminate sheet for cold-bridge blocks, spacers and covers.
Carbon fibre chopped fibre — reinforced compound for brackets, clamps and small fittings.
Aramid filament and aramid fabric — impact, cut and abrasion protection, and vibration damping layers.
Pre-oxidized fibre yarn, fabric and felt — flame-retardant and thermal insulation for hot zones and fire barriers.
Why Engineers Choose Tanchain for Cryogenic Composite Work
Tanchain supplies the full upstream material range that an LNG or cryogenic project needs, from carbon fibre filament and chopped fibre through woven fabric, prepreg, pultruded and filament-wound tube, board and machined parts, to aramid filament and fabric and pre-oxidized fibre yarn, fabric and felt. Sourcing these from one supplier keeps material consistency across a project and reduces the coordination burden between fabricator, insulator and fire-protection contractor.
We work with design and fabrication teams on fibre orientation, resin selection for low-temperature service and the isolating details that prevent galvanic corrosion, so that the composite solution is delivered as a workable, installable system rather than a loose pile of material. If your project involves cold-bridge components, composite supports, lightweight access structures or fire and thermal protection around process equipment, our technical team can help you map components to the right material form and quote accordingly.
To explore the specific products described above, browse our carbon fibre tube, carbon fibre board, prepreg and aramid ranges, or contact us for a quotation and technical guidance on your LNG or cryogenic application.